Five-Axis CNC Commissioning and Acceptance Testing
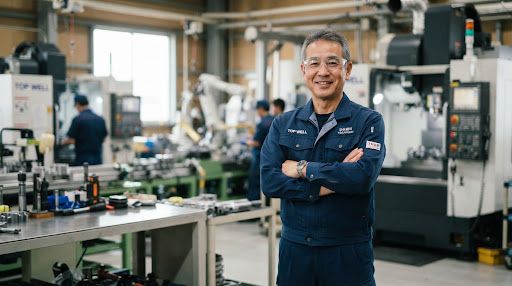
Kenji TakahashiChief Technical Advisor • TOP WELL Industrial Alliance
Share:
Bringing five-axis precision machining centres into heavy industrial production demands strict control of foundation vibration, laser optical alignment and micro-level tolerance inspection. Below is a real technical handover report recently completed by TOP WELL International at the Deep C Industrial Zone in Hai Phong.
HAI PHONG PORT INDUSTRIAL CORRIDOR
Oversized and heavy-lift transport and receipt of precision CNC machines at the Hai Phong deep-water port.
Figure 1.1: The heavy industrial equipment transport corridor and precision mechanical handover by TOP WELL.
1. Industrial requirements and vibration control
Five-axis machining requires a stable installation, controlled operating conditions and repeatable measurement. The commissioning plan should define the equipment requirements before installation begins.
Measurements must be recorded using calibrated instruments and compared with the agreed acceptance criteria. Any corrective work should be verified before production handover.
“Reliable commissioning connects equipment capability with a repeatable operating process.”
— Kenji Takahashi, Technical Advisor
2. A five-stage technical handover process
A structured sequence keeps installation, verification and operator training aligned.
01
Foundation seating and levelling
Check the foundation, lifting plan and machine levelling against the equipment installation requirements.
02
Laser alignment
Measure axis alignment, straightness and squareness using calibrated instruments.
03
Kinematic compensation
Review geometric measurements and apply approved compensation settings to the controller.
04
Endurance testing
Run the agreed test programme while monitoring temperature, vibration and machining stability.
05
Operator training and handover
Provide operating instructions, maintenance guidance and practical training for the site team.
3. Technical acceptance criteria
Illustrative targets below show how an acceptance plan can document measurable requirements. Final values must be agreed for the selected equipment.
Acceptance criterion
Industry reference
Project target
Positioning repeatability
Typical reference: ±0.005 mm
Project target: ±0.0018 mm
Spindle runout
Typical reference: <0.003 mm
Project target: <0.0012 mm at 20,000 rpm
Continuous endurance test
Typical reference: 24 hours
Project target: 72 continuous hours
Technical response time
Typical reference: 24–48 working hours
Project target: under 2 hours in the agreed service area
 7 min read